
What is a Manufacturing Execution System (MES)?
Published:Last updated:Author:Gerry Galloway
Food and beverage manufacturers constantly strive to meet stringent food industry regulations and maintain high quality and efficiency standards. As competitiveness has soared, businesses need to work even harder to find the best way to optimize the production process to stay ahead of their competitors and survive in the market.
Digital solutions, mainly Manufacturing Execution Software (MES), have emerged as critical tools for liaising different supply chain stages, creating real-time visibility and control, and leading to business success.
In this article, we will explore the food MES in detail. We’ll dive deeper into the MES definition, its functionality, benefits, main implementation challenges, and more. If you are looking for a solution to enhance your food manufacturing performance, compliance, and product quality, understanding MES will equip you with the knowledge to make informed decisions.
What Is a Manufacturing Execution System (MES)?
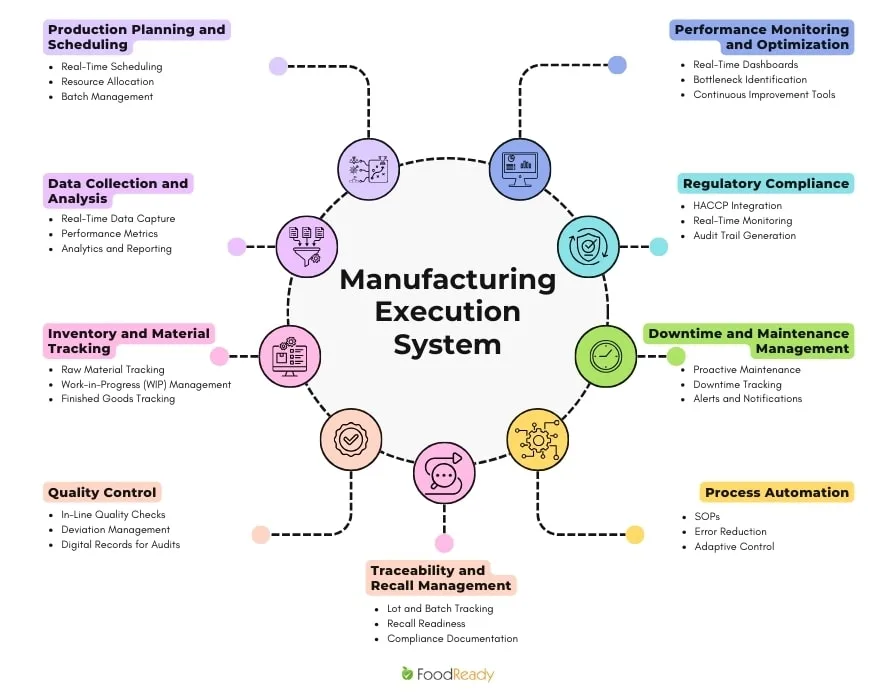
MES stands for Manufacturing Execution System, a software-based solution that helps monitor and control production from raw materials to finished goods, including scheduling, quality, maintenance, logistics, and management. MES joins enterprise-level systems like food ERP or administration and the production floor, including machines and IoT devices.
The manufacturing execution systems (MES) aim to monitor and document manufacturing processes in real time. MES can gather real-time data from different sources and devices, such as equipment and sensors, to give the most accurate overview of the current production state.
With MES, food manufacturers can efficiently manage materials, labor, equipment, and processes, make data-driven decisions, find and resolve potential issues, reduce downtime, and improve product quality.
MES is an excellent solution for enhanced quality control, better traceability, and inventory management. It helps optimize and centralize operations, enabling businesses to allocate resources correctly and bringing faster production and profit growth.
MES is a universal tool that can work in cross-functional environments. It enables comprehensive product lifecycle management, especially in regulated industries like food and beverage.
History of MES
It all started long ago. Manufacturers have always strived to improve their production. The MES concept was formed in the 1990s, and it served as a bridge between the shop floor and management levels and helped optimize operations.
Later, in 1992, a group of software development consultants and solution integrators created the Manufacturing Execution Systems Association (MESA), now the Manufacturing Enterprise Solutions Association. The association established a MESA model - eleven mandatory functionalities that MES applications must have.
MES functionalities developed in the 2000s when the focus was on integrating MES with ERP and other standardization advancements. International Society of Automation developed an ANSI/ISA-95 standard that facilitated the integration of MES by implementing terminology and established activities, functions, and interfaces for manufacturing execution systems.
The fourth industrial revolution has fostered the development of Internet of Things (IoT) technologies, Artificial Intelligence (AI), robotics, cloud computing, and more. MES has improved along with these technologies, so now food manufacturers can benefit from even greater possibilities. The rise of cloud-based MES has enabled quick deployment, flexibility, real-time data access, and seamless integration with other systems, making it a key trend in manufacturing digital transformation.
MES became cloud-based, and implementing them has become much more manageable, making operations even faster. Also, MES integrates with cyber-physical systems, which means MES can combine both hardware and software for enhanced monitoring.
MES can now work with IoT devices, so manufacturing monitoring has become more comprehensive and detailed. With in-depth analytics and AI technologies, MES can better analyze the data received from thermometers and sensors.
Through the years, MES has become an established, more developed, and critical system for food manufacturers, enabling them to receive detailed information for more data-driven decisions.
ISA-95 Levels
The ISA model consists of 5 levels, presenting the place of MES in the manufacturing system:
Level 0 - Physical production process
Level 1 - Involves physical sensors on the shop floor to collect manufacturing data.
Level 2 - Monitoring and supervising where controllers, like a programmable logic controller (PLC), regulate the equipment. At this level, control systems and process control systems are key components, managing both discrete and continuous manufacturing processes.
Level 3 - Manufacturing operations management layer, where you must apply MES.
Level 4 - Business planning through systems like ERP or CRM. At this level, business systems represent the enterprise-level software that MES connects to for integrated manufacturing operations management.
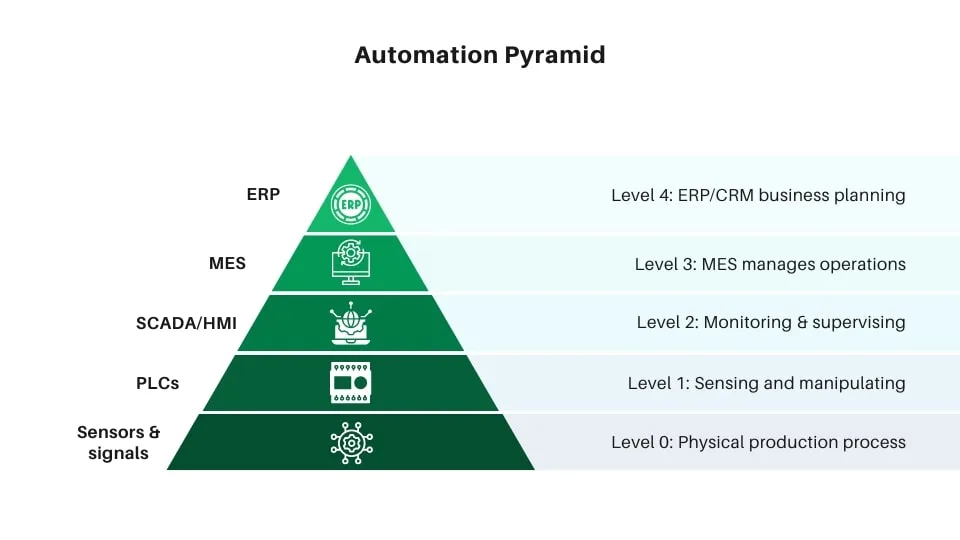
As we can see, MES connects equipment and business administration systems, such as ERP.
How Does MES Work?
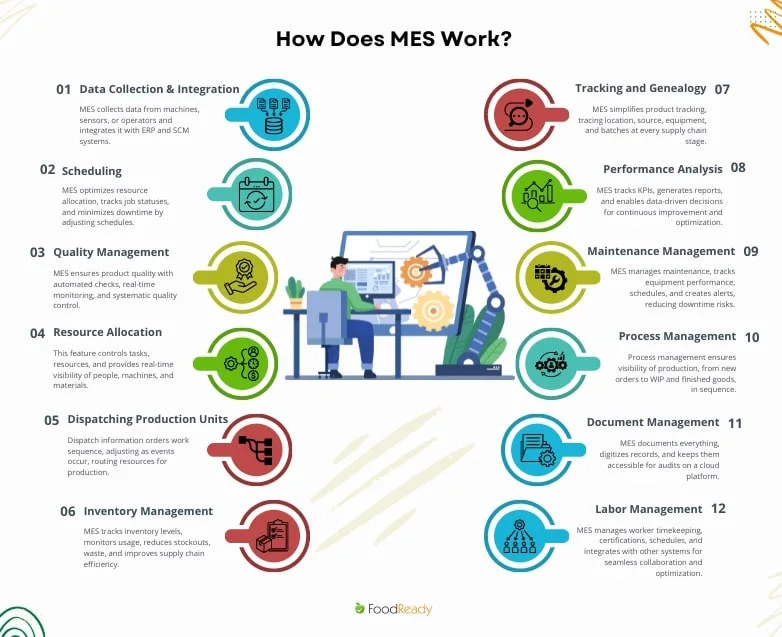
MES functionality can be slightly different depending on the company that uses it. However, it has some established capabilities, so let’s see some core features of MES and how it works:
Data Collection and Integration
MES must collect data from machines, sensors, or operators and integrate it with other systems, such as an ERP (enterprise resource planning) system or SCM (Supply Chain Management). This integration allows a synchronized data flow across the systems.
Scheduling
MES enables efficient resource, equipment, materials, labor, and tool allocation. Its functionality helps accurately track work orders, job statuses, timelines, and related information. You can minimize downtime thanks to the system’s ability to adjust schedules depending on demand, production delays, or available resources.
Quality Management
Another MES capability is ensuring and maintaining product quality. MES can automatically conduct and record quality checks to address and prevent potential issues. Real-time monitoring functionality helps control quality parameters to confirm they meet the standard. Overall, MES will ensure systematic and productive quality control.
Resource Allocation
This feature means controlling what people, machines, and materials should do or where they should go, what is being done now, and what tasks are ready. It provides real-time visibility of resources.
Dispatching Production Units
Dispatch information is an order in which work should be done. The sequence modifies as new crucial events happen. In other words, it means routing the resources to produce a product.
Inventory Management
MES manages inventory level tracking, as the system effectively monitors ingredient levels and tracks product movement and usage. As a result, you will get accurate inventory levels, minimize stockouts or overstock, reduce waste, and boost supply chain efficiency.
Product Tracking and Genealogy
Once you implement MES system, product tracking will be much easier. The system will track and trace the product’s location at any supply chain stage. It will also gather information about the source, equipment involved, lots and batches, etc.
If you’re looking for more information, our complete guide on food traceability is the perfect next step.
Food Traceability
MES helps ensure traceability by tracking raw materials, work-in-progress (WIP) goods, and finished products. This means you can monitor where the ingredients and materials come from, how they are processed, and where the ready product is distributed.
MES provides forward and backward traceability, so manufacturers can track the materials from raw to finished goods and vice versa. With MES, you can be sure that every ingredient is tracked.
MES can also track lots and batches, making it easier to identify the origin and destination of the final product. This is useful when a recall occurs and the affected batch needs to be identified and isolated.
The traceability feature helps promptly respond to recalls, isolate contaminated products, and avoid their further distribution and consumption. As a result, you reduce the damage and save customers' health and your reputation.
Performance Analysis
A manufacturing execution system can help you analyze production performance. It tracks KPIs (Key performance indicators) like efficiency or quality analyses and draws progress reports. Employees can make data-driven decisions to find gaps and areas for improvement, initiate continuous improvement, and develop optimization strategies.
Maintenance Management
MES has maintenance management software features and will help proactively maintain facility equipment. It will track machine performance and maintenance schedules and create alerts and reports. Equipment effectiveness will improve, and there will be fewer risks of downtime.
MES integrations with other systems create a unified environment between manufacturing levels, streamlining maintenance management. MES easily integrates with Industry 4.0 technologies like IoT and AI, and, of course, we should mention other systems like CMMS or food ERP.
Imagine how well MES and CMMS integration can boost food manufacturing maintenance management. While MES covers production operations, CMMS manages maintenance procedures like scheduling.
For instance, suppose MES has detected an issue in a machine's performance. The system instantly triggers the CMMS, which automatically schedules an inspection or maintenance. It can also work another way: MES can modify production if the team notices a problem in CMMS. As a result, you minimize the negative impact on food production efficiency.
Process Management
Process management provides complete visibility over the production processes, including new orders, WIP (Work in Progress), and finished goods. The work will be structured and sequential.
Document Management
MES documents everything it monitors. Moreover, it helps food and beverage manufacturers efficiently manage their records, keeping them accessible when needed, for example, during an audit. On a cloud platform, you can digitize your paperwork and store plans, checklists, instructions, drawings, etc.
Labor Management
You can easily manage the aspects related to your workers: timekeeping, certifications and qualifications, schedules, personnel operations, and more.
Manufacturing execution systems (MES) integrate with other systems, creating a seamless collaborative environment between departments for work optimization and data-driven cross-functional decisions.
Food Safety and Regulatory Compliance
MES helps meet food safety requirements, including HACCP, FSMA, FDA, ISO, etc. It will also make it easier to prepare for food safety audits. The system enables real-time data collection, record-keeping, monitoring, etc., which are essential for regulatory compliance.
You will benefit from automatically generated reports, which provide a detailed overview of certification processes, compliance checks, or audits. These reports ensure you can access all the documents you need.
MES records all actions during production, including quality control checks, equipment maintenance, etc., keeping a consistent and comprehensive audit trail. By recording preventive maintenance actions, MES helps maintain equipment compliance.
Corrective and preventive actions are also under MES control. Whenever an issue arises, MES incorporates an integrated CAPA system to address the incident as quickly as possible. With a manufacturing execution system, you will tackle a problem before it escalates.
Overall, MES aims to help you maintain and improve food safety compliance during production.
Integration Capabilities for Better Results
The MES system can work with other enterprise systems, enabling a more complex approach and seamless communication on different company levels, which is critical for the highly regulated food industry.
MES can integrate with an ERP system, streamlining order management, improving production planning, enabling real-time transparency, optimizing inventory, and more. Integrating MES+QMS can also enhance quality processes and upgrade monitoring by integrating IoT devices.
Speaking about ERP, if you are still questioning what is better, ERP or MES, our new blog can help you.
Integrations create a unified environment, making food production more efficient and eliminating blind spots that could cause downtime, errors, and financial losses.
They make manufacturing processes more visible. The system monitors and controls production activities from raw materials to the end product to find potential issues as they arise. Accordingly, once a problem is identified, immediate corrective actions can be initiated.
Let’s say one of the conveyors has broken down. MES gathers the data and alerts the worker in charge to handle an issue quickly.
By leveraging MES capabilities like real-time monitoring, quality control, process and progress management, labor management, and others, food manufacturers will significantly improve their performance, maintain food safety compliance, and maintain efficient and seamless workflows.
How MES Optimizes Food Production Planning and Scheduling
Food manufacturers know how vital production planning and scheduling are for maintaining food safety and quality and complying with stringent regulatory requirements. Manually doing that or using an outdated system is an unnecessary challenge. Is there a solution?
On the one hand, the answer is simple – a manufacturing execution system (MES) is what you need to revolutionize food production planning and scheduling in your business. On the other hand, implementing it into reality is a bit more complicated.
What Are the Challenges of Food Production Planning and Scheduling?
Food manufacturers can face various challenges during the production planning and scheduling processes.
Awareness of these obstacles is crucial, but MES software can help resolve them.
1. Regulatory Compliance
Inefficient scheduling and production errors complicate compliance with stringent food safety standards, such as FDA, FSMA, USDA, etc. You need a structured system to avoid consequences of noncompliance, such as food safety risks, recalls, and penalties.
2. Demand Fluctuations
Production planning can be a hurdle when you face variations, such as seasonal demand, rapidly changing consumer trends, or unpredictable market changes.
3. Ingredient Shortages
Sometimes, food manufacturers face raw material and ingredient shortages caused by supply chain disruptions or unstable product availability. This can delay production schedules.
4. Shelf-Life Constraints and Expiry Management
You must control strict timeframes within which perishable ingredients and finished products must be used or consumed. This is a must to prevent spoilage.
5. Unexpected Downtime
Equipment downtime can lead to significant schedule delays as it intervenes in production. Moreover, machine failure causes extra maintenance costs.
6. Production Bottlenecks
Failure to synchronize multi-stage processes, such as mixing, cooling, or packaging, can cause delays and disruptions.
7. Handling Batch and Recipe Variability
Production schedules become tricky when managing food products with different cooking times, unique recipes, and processing stages. Plan carefully to avoid failed timings, production mistakes, or ingredient shortages.
8. Changeover Management
If a manufacturer handles custom orders, produces food in smaller batches, or frequently switches the recipes, they may face a challenge when making schedules due to different products requiring different ingredients, equipment settings, or processing times.
How Does MES Improve Production Planning and Scheduling?
MES has multiple features that will assist you while planning and scheduling your production processes. Let's take a look at them:
Real-time Data
MES functionality includes real-time data capture from the production floor. This lets you obtain information about material usage, machine performance, labor availability, production progress, etc.
This way, you can make informed and timely planning and scheduling decisions based on actualized data.
Automated Scheduling and Resource Allocation
MES software optimizes resource allocation, such as raw materials, by analyzing demand forecasts, inventory levels, and other factors. The system also helps easily assign tasks and materials to minimize bottlenecks.
With the real-time data, MES creates opportunities for fast and automated scheduling.
Integrations With Other Systems
MES integration capabilities are impressive! The system can integrate with Enterprise Resource Planning (ERP) and warehouse management systems (WMS), ensuring visibility and connection between different production layers.
This way, you align production schedules and streamline operation flow by preventing overproduction, stockout, and other issues.
Predictive Maintenance
MES optimizes maintenance by integrating computerized maintenance management systems (CMMS) and enabling predictive maintenance scheduling.
This way, MES helps manufacturers identify potential downtime and guarantee uninterrupted production flow.
Batch Processing and Recipe Management
Managing versatile recipes, cooking times, and other specifics is challenging. MES enables efficient recipe management and batch processing to ensure consistency and product quality.
This feature lets you control formulas, times, different-sized batches, special orders, and other crucial factors to avoid delays and mistakes while planning production.
Compliance Management
As we already know, compliance with stringent regulations is complicated, but MES software is excellent for this purpose.
The system helps adhere to regulations such as the FSMA 204 rule by integrating traceability and batch management to track ingredients in the supply chain.
This is not the only compliance-related feature. MES is crucial for quality management and helps control allergens, manage documentation, and cover other aspects needed for maintaining compliance.
Real-time Monitoring Notifications
MES's real-time alerts help you make proactive decisions and timely changes if needed. MES will notify you when there's an equipment issue, schedule changes, etc.
You get an instant update on things happening on the production floor without even walking through it and checking manually. The system monitors the production so you don't waste time and can concentrate on other tasks.
Results of Using MES in Food Production Planning
Once you successfully implement a Manufacturing Execution System, you'll see a positive impact on planning and scheduling procedures. These improvements will include:
- Better resource utilization and allocation
- Faster response to fluctuations
- Minimized downtime
- Regulatory compliance and audit readiness
- Better productivity
- Cost and waste optimization
What Are the Trends in MES for Production Planning and Scheduling?
Trends in MES are emerging rapidly, and you don't need to be scared or skeptical about them. Instead, use them in favor of your business to streamline production planning and scheduling.
Artificial Intelligence
AI and machine learning transform predictive scheduling. AI-driven algorithms can use historical data, demand patterns, and real-time production insights to generate optimized schedules.
Cloud Computing
Cloud computing is a rapidly growing trend in food manufacturing. AI-driven algorithms can use historical data, demand patterns, and real-time production insights to generate optimized schedules. According to a report by Next Move Strategy Consulting, the industrial cloud computing market size is expected to reach $1,094.62 billion by 2030, compared to $311.75 billion in 2023.
Many manufacturers are shifting to cloud MES as it gives more flexibility and remote accessibility. Cloud systems enable more seamless scheduling and collaboration across facilities.
Sustainability
Nowadays, sustainability and waste reduction are priorities for different industries. With MES, you can track waste and incorporate eco-friendly scheduling features. You can also optimize batch sizes and resource utilization to minimize food waste and energy consumption.
IoT Devices
Internet of Things devices are boosting real-time data collection. Sensors monitor information, including equipment performance, ingredient levels, and environmental conditions. As a result, the insights provided will optimize production schedules dynamically.
Keeping up with industry trends will help you stand out and enhance your production planning and scheduling algorithms with MES.
Why Is MES Essential for Quality Management?
Ensuring product quality is necessary in a regulated and competitive food manufacturing industry, as any quality deviations can lead to costly recalls, noncompliance, and damage to brand reputation.
The Role of Quality Management in Food Manufacturing
Quality control in the food industry means testing food products for adherence to specifications and potential deviations. The quality check can relate to food safety, nutritional value, or other qualities.
A proactive approach to quality management is an indispensable part of the food manufacturing process. Producers want to make their products reliable and safe, and proper quality management lets them achieve that.
High-quality products defend the company's reputation and reliability, improving customer satisfaction and trust. Moreover, ensuring product quality boosts efficiency and profitability. A proactive approach to quality significantly reduces food safety risks.
MES and QMS are connected, and quality management is one of the features of the manufacturing execution system.
Let's break down the main points of why you need MES for quality management.
1. Real-Time Quality Monitoring
Maintaining consistent quality requires regular checks in fast-paced and regulated food manufacturing. MES stands out for its real-time data collection and monitoring capabilities. The system helps oversee and analyze product quality and address issues instantly.
Manufacturing Execution System software will enable you to continuously track and collect essential quality metrics, such as temperature, humidity, ingredient weights and proportions, and equipment performance. Moreover, MES can easily visualize data with real-time dashboards displaying key quality indicators.
Real-time monitoring guarantees that you will find potential issues as soon as possible, minimizing their impact on product quality and fostering a proactive quality control environment.
2. MES Reduces Human Error in Food Production
Human error is a frequent cause of quality issues, noncompliance, production delays, and other problems. In fact, 80-90% of accidents in different manufacturing fields are caused by human error.
Of course, we are all people and can make mistakes, but we can implement technology to avoid this problem and ensure product quality.
MES software automates the processes and repetitive tasks where people are prone to making unintentional mistakes. Manual processes are time-consuming and depend on the workers' attention and state.
MES streamlines and digitizes many processes. For instance, it automates data collection and provides digital work instructions.
Overall, MES saves time and reduces the chances of mistakes or missed spots. In the meantime, personnel can switch their focus to tasks that require human input.
3. Improved Food Traceability
Food traceability is essential to a quality management system in food production, and MES can help you build a robust traceability system. Efficient product tracking will significantly reduce recall risks and minimize food contamination. Moreover, it will help react quickly to potential food safety issues.
Speaking in more detail, how does MES improve traceability?
Batch and Lot Tracking: MES can track lots and batches of raw, semifinished, and finished goods.
Digitized Documentation: With MES, you can create a centralized database and eliminate paperwork. Digitized recordkeeping is a huge plus when you need to log every step of production in real time.
Real-Time Data Integration: MES can integrate with sensors and other equipment to collect data, such as raw material origin, production settings, or distribution details.
Forward and Backward Traceability: A manufacturing execution system will help you trace issues backward and forward to ensure efficient product recall or incident investigation.
Integrations With Supply Chain Management Systems and ERP: MES can connect with food ERP and supply chain management systems, which will help create a single picture of production and distribution.
MES has versatile integration capabilities; another great option to improve quality management is integrating it with QMS.
4. The Impact of MES and QMS Integration
You can connect QMS and MES to enhance production and quality management. Both systems have powerful features, and leveraging them can help you produce high-quality foods. Combining two systems will ensure real-time visibility, efficient quality control, centralized data management, and food safety compliance.
In addition, you will streamline nonconformance management. The integration will let MES flag deviations and QMS manage nonconformance reports, making QMS an even more powerful tool for ensuring that production complies with the latest food safety and quality standards.
MES-QMS integration will bring various advantages, including enhanced product quality, compliance with food safety standards, such as HACCP, GFSI, and FSMA, improved efficiency, etc.
5. Enhanced Standardization Across Processes
MES creates a centralized framework to drive uniform processes in production. How does MES do that?
The system digitizes work instructions, minimizing paper-based and memory-dependent processes. It enables workers to access real-time and tailored task instructions.
MES ensures that ingredients, formulas, and recipes are consistent and accurate, preventing errors and quality deviations.
Monitoring CCPs (Critical Control Points) also becomes a breeze as MES automatically monitors them to ensure compliance with quality standards.
Integrations with equipment help MES ensure that critical parameters, such as temperature, pressure, humidity, etc., are set correctly.
6. Integrated CAPA Management
Deviations, malfunctions, inconsistencies, and other issues can undermine food safety and quality in the food and beverage industry. Proper and timely corrective and preventive actions can be a life-saver.
A Manufacturing Execution System streamlines CAPA processes, making them more efficient. As a result, you successfully address issues occurring in food manufacturing.
MES supports CAPA by ensuring monitoring and reporting, automating deviation and incident detection, centralizing documentation, implementing root cause analysis, and preventive actions.
MES-enabled CAPA improve accuracy, ensure food safety and quality compliance, and enable faster response times. Moreover, historical MES data helps prevent potential issues before they even occur.
7. Root Cause Analysis Made Easier
Root cause analysis (RCA) is essential for identifying the underlying causes of quality issues in food manufacturing. By conducting an efficient RCA, manufacturers can find the initial cause of a problem and implement corrective actions.
A Manufacturing Execution System boosts RCA by providing detailed historical data and other tools to identify and resolve problems. What are these tools? How does MES support root cause analysis?
Data Centralization: MES collects and centralizes data from the equipment, production lines, and sensors, making it easier to trace an issue.
Automated Report Generation: MES provides real-time insights into problems, indicating the affected batches, equipment involved, and time.
Process Mapping: MES gives you a detailed overview of workflows so you can trace an issue back to its source.
Real-time Notifications: instant alerts provided by MES help the team identify potential causes of an issue faster.
As a result, MES for RCA brings many benefits, including faster and more accurate problem identification and resolution, improved compliance, and better preventive measures, leading to increased product quality.
8. Predictive Maintenance for Better Quality Control
Equipment state and performance significantly influence the food quality. Equipment failure can cause quality issues, such as food contamination. Predictive maintenance helps predict and prevent potential problems before they cause disruptions.
MES facilitates predictive maintenance by enabling real-time equipment monitoring, data-driven insights, and automated alerts. In addition, MES can integrate with predictive maintenance systems, such as CMMS, which also streamlines equipment maintenance.
MES-enabled predictive maintenance helps switch from reactive problem-solving to proactive prevention. This way, you can achieve consistent product quality, improve food safety, and reduce unplanned downtime and costs.
Transform Data Into ROI With MES
Stop flying blind. MES delivers the actionable insights your facility needs to improve quality, reduce downtime, and meet audit standards.
How MES Data Drives Better Decision-Making
In a highly competitive and regulated food industry, data-driven decisions are a powerful tool for manufacturers. Data accessibility and speed in making decisions have become crucial in the context of Industry 4.0, smart manufacturing, day-to-day compliance, and efficiency.
MES industry statistics show that 70% of companies state that implementing a manufacturing execution system (MES) has led to enhanced decision-making capabilities. Indeed, MES drives digital transformation in manufacturing and revolutionizes decision-making by enabling more accessible data collection and processing.
What Is Data-Driven Decision-Making in the Food Industry?
Data-driven decision-making (DDDM) means making business decisions regarding production, operations, customer satisfaction, supply chain, and other aspects after having analyzed given facts and metrics to adhere to business strategies and vision.
For this purpose, decision-makers can gather data from various sources, such as performance reports, analytics, actionable insights, customer feedback, etc.
The Role of Data-Driven Decision-Making
Each decision has its own outcomes, and food companies want them to be positive. Data-driven decision processes drive work optimization, profit growth, a strong reputation, and reduced costs, and that's not even the end of the list!
The food industry is strict and demanding, so leveraging real-time data is critical to compliance and success. Moreover, the strategy will help filter the information flow and get the verified data. This is why you need MES data for decision-making.
How Does MES Help Make Better Decisions?
One of the most outstanding MES benefits is informed decision-making. In addition to digitized operations and streamlined production, you will get maximum transparency and ease when making tough choices (and not only).
For example, world-leading food companies such as Danone, Mars, and Kraft Heinz utilize MES data for decision-making. The system enables real-time data collection on regulatory compliance, quality, production performance, etc. It helps them react promptly to issues, achieve production transparency, and make timely decisions. Sounds fascinating? Let's see how it works!
1. MES Provides Real-time, Accurate Data
Manufacturing execution systems collect data in real time from different sources, such as equipment or human activities. Together, they enable decision-makers to get a complete picture of what is happening in place and consider all the crucial aspects of production.
What's more, the data updates constantly, enabling information flow that helps keep up with the changes, improve uptime, and minimize mistakes. The world is changing at an insane pace, and so is the food industry with its regulations and trends. MES helps you stay tuned and find the right solutions.
2. MES Enables Predictive Analytics
Looking ahead is as critical as considering existing facts. The data collected by MES also serves as a tool to predict future trends, risks, and opportunities. Predictive analytics by MES will enable better planning, scheduling, and more precise inventory management.
You will be more sure about future actions and won't waste time assuming and guessing. What can be better than awareness in further actions?
3. The System Helps With Food Safety Compliance
MES features help comply with local and state regulations. This helps you stay up-to-date with the latest requirements and drive compliance-oriented decisions. You will know how to act according to food safety standards.
Compliance is crucial for food and beverage manufacturers, and MES helps gather information to ensure adherence to every aspect of food safety and quality.
4. MES Centralizes Data
A manufacturing execution system synchronizes all the processes and lets you manage everything from one platform. You will no longer have to juggle multiple informational sources and will be able to process information efficiently with centralized real-time data.
Avoid wasting time and attention on unnecessary actions when trying to find the needed source. Simplicity and unity are key.
5. MES Integrates With Other Systems and Devices
You will also benefit from MES integration with ERP systems, Supply Chain Management, or IoT devices. Integrated systems and equipment facilitate and boost information exchange and synchronization on different levels, again making you more capable of making effective decisions.
Smart manufacturing goes beyond a single platform and leverages integrated systems like MES, ERP, or IoT devices to ensure efficient, real-time data collection, enable real-time production monitoring, and eventually enhance decision-making.
As a result, food manufacturers will optimize their production, avoid mistakes, manage issues quickly, and achieve production line transparency.
6. MES Fosters Better Communication
Poor communication can lead to misunderstandings, lack of information, and other professional failures. MES fosters better communication and collaboration between workers at different levels and departments to facilitate data exchange.
7. Real-Time Analytics and Reporting Are Key
Real-time analytics in food manufacturing is essential. The manufacturing execution system will always keep you updated. Its comprehensive analytics and reporting features will help you stay current and make evidence-based decisions.
8. MES Automates Processes in Food Production
MES automates the workflow, taking over tedious and time-consuming tasks so that you can focus on more critical questions. Moreover, it will make the process error-proof and faster so you can get the work done more quickly and of better quality.
How MES Helps Food Manufacturers Minimize Scrap?
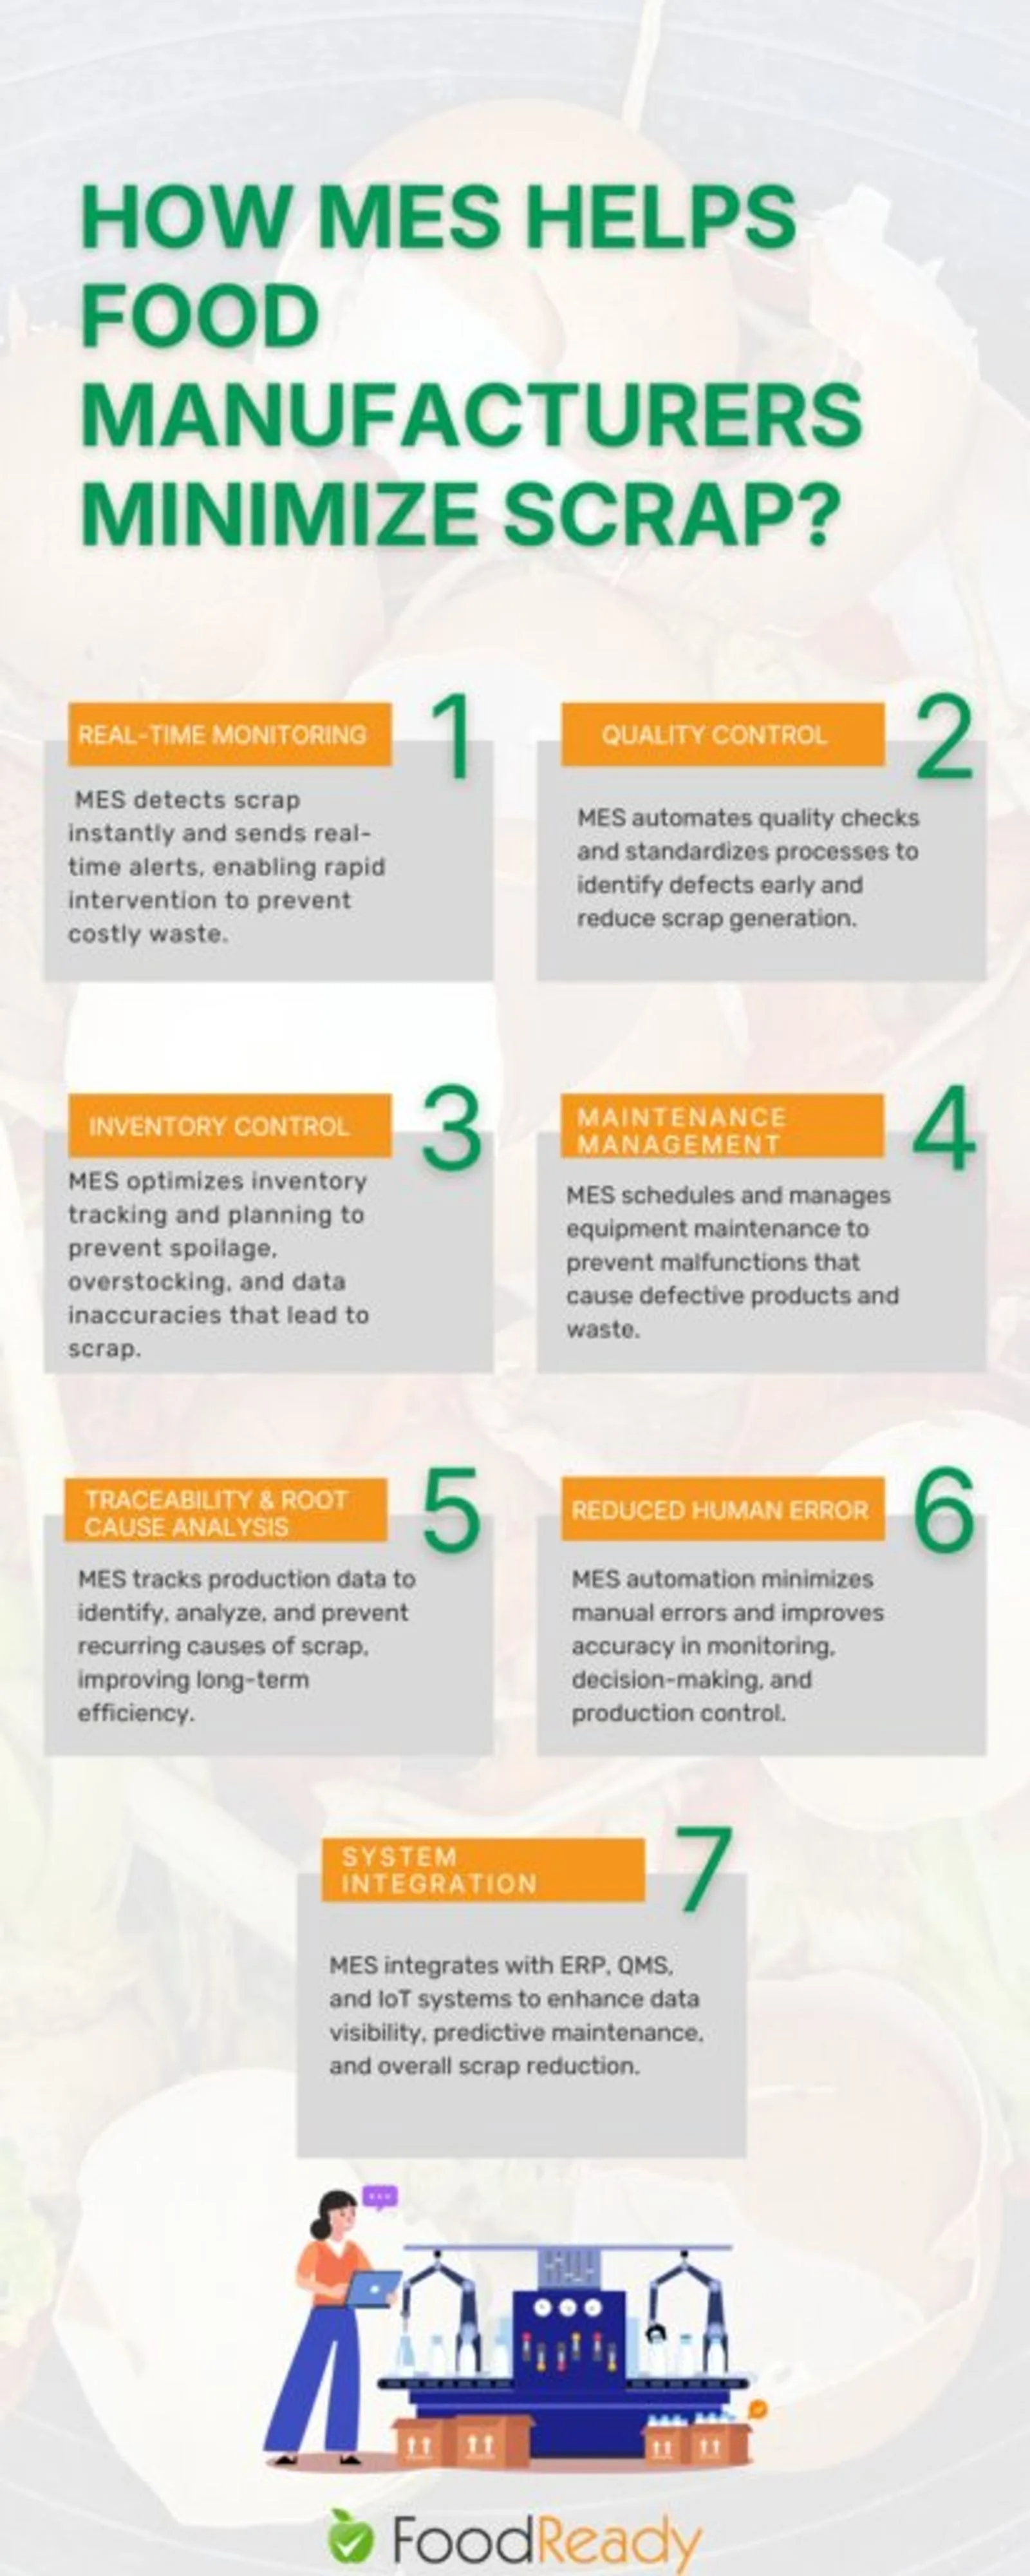
MES has many benefits, but we haven’t mentioned one yet: scrap minimization. Implementing MES software will help you reduce waste thanks to features like real-time data management, quality control, traceability, maintenance management, and others. Let’s take a deeper look at each aspect.
1. Real-Time Data Monitoring and Notifications To Minimize Production Scrap
MES is well-known for its monitoring and data collection capabilities. It’s almost impossible to catch inconsistencies and extra scrap manually and instantly. You will need some time. MES will notice scrap faster and immediately notify you about the problem.
Real-time tracking and control make you feel more confident about catching the most minor details as fast as possible. As a result, you avoid expensive waste.
2. Quality Control for Scrap Reduction
Quality control measures are essential for reducing scrap material, and the MES quality management feature can assist with this task. The system will automate the quality checks and help with process standardization. Proper quality control procedures will help you catch the issues early to reduce the scrap amount.
3. Inventory Control To Avoid Scrap Inventory-Caused Scrap
Some inventory-related problems can lead to extra scrap in manufacturing. These could include poor planning, spoilage, overstock, inaccurate inventory data, etc. The MES inventory management feature can help handle these issues and ensure real-time inventory tracking, optimize production schedules, establish shelf-life control, and more.
The feature will help optimize inventory to minimize waste and scrap caused by inventory inconsistencies.
4. Reducing Equipment-Related Scrap With Maintenance Management
Poor equipment maintenance is another cause of scrap. Machine malfunctions can lead to low-quality or defective food, which causes extra waste. MES functionality allows you to manage equipment maintenance, helping you avoid downtime and product defects and minimize scrap on the production floor.
5. Traceability and Root Cause Analysis for Better Scrap Management
MES traceability helps businesses track production processes forward and backward, helping catch issues in production, minimize loss, and identify spoiled products. It allows manufacturers to find the root causes of scrap and incorporate preventive measures.
The manufacturing execution system catches deviations, and then you can analyze the problem using the system’s historical data.
Identifying the root cause will help significantly reduce scrap, ultimately increasing efficiency and productivity. Even more important is that you can archive the issue in the system, and if a similar problem occurs, you will find a way to deal with it faster.
6. MES Reduces Human Error
MES automates the production process, significantly lowering the chances of human error and missed blind spots. Manual tracking is time-consuming and less effective than implemented MES software. Monitoring the food inventory, catching mistakes, and making data-driven decisions will become more manageable with a digital solution.
7. Integration Capabilities Drive More Efficient Scrap Control
MES integrates with other production systems, such as Enterprise Resource Planning (ERP), Quality Management System (QMS), or Food Inventory Management Software, to enhance scrap reduction efficiency.
In addition, MES uses IoT technology to retrieve data from machinery, which improves predictive maintenance and helps reduce scrap caused by faulty equipment.
Integrations help create a unified ecosystem, assisting manufacturers to oversee production operations better. Real-time visibility and proactivity will help minimize scrap and waste.
Scrap Reduction Starts with Real-Time Insight
Get visibility into your entire shop floor with MES software that catches issues before they cost you.

Dashboard
Cloud-Based MES vs. On-Premise MES
MES can be different; for instance, there are more traditional on-premise platforms and modern cloud-based systems. Your perfect choice will depend on your needs, goals, and other factors.
What Is a Cloud-Based MES for Food Manufacturers?
Сloud MES is a software as a service (SaaS) solution that optimizes manufacturing operations using cloud technology. The system is hosted on remote servers and is accessible via the Internet. You can subscribe to a cloud MES, and third-party software providers will manage it for you.
A cloud-based manufacturing execution system is easily scalable, secure, available remotely, provides real-time updates, and has other features and benefits that we'll discuss later.
What Is an On-Premise MES for Food Manufacturers?
On-premise MES works within the company's IT infrastructure on local servers. The system offers data security and total control. This type of MES will guarantee that sensitive data stays in the facility. On-premise MES works seamlessly without an internet connection and can be easily customized for the company.
Both system types will help guarantee food safety and compliance for food manufacturers and maintain efficiency, but let's take a deeper look at some aspects to see the strengths and weaknesses of each solution.
Comparing Cloud-Based MES and On-Premise MES
Both cloud and on-premise MES solutions have peculiarities, and comparing them will help understand what is better in a particular case. Some key aspects to compare are cost, access, security, regulatory compliance, etc.
1. Costs
- Cloud MES is subscription-based. The provider hosts and maintains the software, so the initial cost is lower, and you don't pay for the hardware or infrastructure.
- On-premise MES requires a more significant upfront investment. This can include paying for hardware and software, licenses, maintenance costs, and salaries for the IT team.
2. Access
- A cloud-based system is accessible from anywhere if you are connected to the internet.
- On-premise software is available in the company's local network.
3. Security
- Cloud MES software stores data in a cloud storage system, which involves third-party hosting. To protect sensitive data and guarantee confidentiality, cloud MES provides comprehensive security measures, such as multifactor authentication, complies with security audits like SOC 2, and offers disaster recovery.
- An on-premise MES solution offers high data control, keeping it safe and secure within the company's local servers. However, on-premise systems can be vulnerable to internal security risks and require well-developed internal protocols to prevent these issues.
4. Food Safety and Regulatory Standards
- Cloud MES doesn't ensure compliance itself, but it provides tools and updates to align processes with regulations. The user must implement these updates manually.
- On-premise systems are also great for maintaining food safety and regulatory standards. However, they don't support automatic data updates unless the software is paired with appropriate external integrations to automate them. In another case, the IT and compliance teams must stay informed about regulatory changes and manually update the system and processes.
5. Deployment
- Cloud software is quick and easy to deploy, as cloud MES specifics help avoid time-consuming installation. However, some factors, such as data migration complexity, can slow the process.
- Implementing the on-premise system requires time and effort to set up the infrastructure.
6. Scalability
- Digital MES is easily scalable, provides instant updates, and is flexible overall. Cloud hosting enables growing food businesses to expand the system's capabilities without investing in hardware and infrastructure modifications.
- On-premise MES can scale by expanding infrastructure and adding hardware, which can take longer than cloud systems.
7. IT and Maintenance
- Cloud manufacturing execution systems are hosted by the provider with the most IT responsibilities. MES vendors also control automatic updates and maintenance.
- If you choose on-premise software, you need a dedicated IT team to oversee MES maintenance and updates.
8. Customization Capabilities
- The level of customization depends on a system and vendor, but many modern cloud MES solutions provide APIs, modular features, and other tools that make them highly customizable.
- The on-premise solution is highly customizable, as food businesses can fully control the software's infrastructure. This allows them to tailor the solution as needed.
9. Reliability
- Digital MES is highly reliable. The software has sophisticated hosting environment and failover systems. Cloud MES vendors offer Service Level Agreements to guarantee 99% uptime.
- On-premise MES works on its infrastructure and doesn't rely on external providers or the Internet. The software only depends on the robustness of the internal IT infrastructure. It's an excellent solution for manufacturers who must work without interruptions.
Aspect | Cloud-Based MES Software | On-Premise MES Software |
Total Cost | Subscription-based with lower initial costs. | Requires significant upfront investment. |
Accessibility | Available from anywhere with internet access. | Accessible within the company's local framework. |
Data Security | Third-party hosting. Comprehensive security measures to protect the data. | High-level data security, as the information is stored on local servers. Internal security threats are possible without proper protocols. |
Impact on Regulatory Compliance | Provides tools and updates to support compliance. Users ensure that regulatory requirements are implemented well. | Requires manual monitoring of regulations and updates to ensure compliance with food safety standards. Integrations can help automate the process. |
Deployment Complexity | Quick and easy to deploy. | Requires time to implement. |
Scalability | Easily scalable. | Scalable but depends on additional IT resources and hardware. |
IT and Maintenance | Hosted and maintained by the provider. | Requires an IT team in place. |
Customization | Customizable thanks to APIs and modular features. | Highly customizable. |
Reliability | Very reliable, provided that there's a stable internet infrastructure and a backup system. | Highly reliable, works independently of the internet. |
When To Choose Cloud or On-Premise MES?
Choosing between cloud and on-premise MES will depend on several factors, such as your business needs, objectives, and regulatory requirements. You can compare some key aspects:
Cloud MES Software is suitable for:
- Small and medium food businesses and startups limited in budgeting and IT resources.
- Geographically distributed companies and facilities that still need real-time MES data.
- Remote teams.
- Food manufacturers who want to scale up quickly and without significant investment.
- Those who have less time and want to implement MES faster.
- Companies who maintain business continuity and want to store data in the cloud in case of failures or unplanned issues.
On-premise MES software is perfect for:
- Those with advanced security needs who can't expose data to third parties.
- Food companies that need comprehensive customization.
- Manufacturers with unstable internet connection.
- Have an IT team in place to maintain MES.
- Those who want to avoid costly downtime and don't want to rely on external factors like internet outages.
How To Decide What MES To Choose? Key Questions to Ask.
Making an informed decision about what kind of MES software to use is vital, as it can influence further performance and efficiency. When choosing, ask yourself several questions to help you decide.
- What Is My Budget? Compare cloud and on-premise MES pricing and think which solution will fit your financial plan.
- Do I Need a Solution With Remote Access? You might need a cloud MES if you have multiple-location production and remote teams. Otherwise, if your operations are centralized, you can choose either an on-premise or cloud MES, depending on your preferences and other factors.
- Do I Have/Need an IT Team To Manage On-Premise MES? You can choose the on-premise MES version if you have dedicated personnel or are ready to hire new people. Cloud MES is great if you don't have an IT team and want a third party to manage the system.
- What Level of Security Do I Need? Choose cloud MES if you trust third-party vendors and opt for an on-premise system if you must control sensitive data fully and independently.
- Does My Company Plan To Scale? If you are a growing business, cloud MES will quickly adjust to you, and this is what you need. If you don't plan to scale, you can also think about on-premise MES.
- How Much Time Do I Have to Implement a Solution? The cloud version is the best if you need to deploy MES faster. On-premise MES will take longer to implement, so it will fit companies that can devote the time required for this purpose.
- Do I Need To Customize MES? Cloud systems are ideal for businesses that need moderate customization and value flexibility. However, companies with highly specific workflows will benefit from on-premise MES due to their extensive level of customization.
- What If I Can't Connect to the Internet? Of course, modern technology reduces the risks of internet downtime, and cloud systems are typically very reliable. However, if you are still unsure whether the connection is good enough, on-premise software can be a solution.
This questionnaire will help you better understand your needs, but you should also remember your specific requests. Proper analysis is critical. If you need help, address the providers you are considering, and they will consult you. For instance, at FoodReady, we offer a demo and a profound consultation for potential clients.
Implementing MES Into the Food and Beverage Business
Engaging a manufacturing execution system is a complex but structured task. Here are steps to successfully implement MES system into your food and beverage business.
Plan and Assess
Before implementing a manufacturing execution system, you must assess the scope, goals, and requirements. You must also understand how ready the company is and identify the gaps in the current system.
Choose What MES Software You Want
You need to decide what software provider you want. Research and compare different MES software solutions. The criteria for the comparison could be affordability, compatibility, functionality, scalability, user-friendliness, features, etc. Check for feedback to see real cases of software usage.
Prepare the Plan
You must develop an implementation strategy, create a project plan, and involve stakeholders, including the IT team, management, quality control team, etc. To successfully implement MES, use a standardized methodology, such as Scrum. The team must be on the same page and understand the process’s structure. This will facilitate the process.
Prepare the Environment
Ensure the software is compatible with existing systems and that your IT infrastructure supports it. You may need to update data security terms or upgrade the hardware. Make sure the software can integrate with existing systems, such as ERP, and that it meets your specific requirements and fits the workflow.
Data Transfer
Data migration includes moving existing data, such as production data, inventory and quality records, reports, etc., to the MES.
Training
Ensure that all employees working with MES are educated on how to use the software. Most software nowadays is user-friendly, so the intuitive interface will help workers quickly learn the ropes.
Implementation
Now, you need to test the system carefully. Once you see no issues, you can deploy the software.
Continuous Improvement
The food industry and technology evolve, so after implementing manufacturing execution system, you must constantly monitor its performance and upgrade it according to the latest food safety regulations and technological advancements.
Implementing new software can be daunting, but it’s worth a try, as MES improves quality, streamlines the production process, and brings many other benefits.
How Can Food Companies Benefit From MES?
MES brings significant advantages to different aspects of food manufacturing, including machine process control, recipe management, traceability, and more. Let’s look at how MES solution can benefit your food and beverage business.
Visibility and Efficient Production
MES helps you reach transparency in production, boosting efficiency and productivity. You can handle large volumes of information in one system that analyses it for you. It helps increase performance, quality, and availability.
MES Makes Production Error-Proof
MES ensures automated workflow, monitoring, and analysis, which helps companies reduce waste and allocate resources correctly. It will also help minimize human factors that can lead to costly mistakes.
Enhanced Inventory
A manufacturing execution system makes inventory management highly precise, outperforming any other system. MES can track raw, finished, and semifinished goods in the supply chain and transfer the information to an enterprise resource planning (ERP) system. As a result, you will improve traceability and supply chain efficiency.
Improved Traceability
Traceability is critical in the food and beverage industry, especially nowadays, when many companies must comply with the FSMA 204 traceability rule. MES will significantly streamline inventory management, helping you comply with food safety regulations.
Better Communication
MES transfers information to the right place, at the right time, and to the right people. Its level 3 position in the ISA model described earlier makes it a great mediator between the ERP and production. This means that no valuable information will be lost in the manufacturing process.
Cost-effectiveness and Efficiency
Having implemented MES system, you will no longer spend extra time on manual data management. It will provide you with more resources for other tasks that require your time. So, MES integration leads to optimized time management and better efficiency.
Continuous Improvement
Continual improvement is an essential part of the food and beverage manufacturing process. Food companies will find growing and maintaining consistent quality easier with better transparency and optimized data exchange.
Overall, the manufacturing execution system has many benefits, and each food manufacturer can find even more, depending on their request. Considering the pros and cons of MES will help make an informed decision.
Increased Food Safety
MES will help you ensure that your food meets the latest food safety standards due to established quality control and monitoring measures. You will get a better overview of the process, enabling better capture of food safety hazards.
Guaranteeing food safety is a complex procedure, and MES software will let you streamline all the steps, which makes it less likely to miss a blind spot.
Regulatory Compliance
Technologies are fundamental to ensuring regulatory compliance with local, state, and international regulations. MES will automate compliance with the FDA, FSMA, or HACCP standards due to an organized documentation system in your facility.
Predictive Maintenance and Reduced Downtime
You can integrate MES software with predictive maintenance or machine learning tools to monitor equipment health. This way, the system will collect data and help anticipate potential breakdowns. By ensuring smooth equipment performance, you will improve uptime, stay assured that your production runs effectively, and have a higher chance of meeting compliance standards.
Improved Operations
Productivity is vital for any business, and the manufacturing execution system is here to make your business as efficient as possible. The system streamlines and optimizes the production process and helps you avoid delays or losses.
A good example of optimizing operations with MES is Coca-Cola. The beverage giant relies on MES to optimize its bottling operations globally. The system provides comprehensive visibility into production metrics, enabling Coca-Cola to identify and resolve bottlenecks swiftly, maintain consistent product quality, and achieve faster changeovers between different product lines.
Audit Readiness
Audit preparation will become easier once you have an MES. The software provides reports and monitors the process, enabling more quality audit preparation. As a result, you will pass regulatory audits like HACCP, GFSI, and others.
Moreover, once you prove regulatory compliance, you will increase customer satisfaction and improve your position on the market, as long as certifications pave the way for recognition and impeccable reputation.
Better Decision-Making (Benefit Summary)
MES strives to improve decision-making. The software will help you achieve maximum transparency and overview, making it easier to decide on essential questions. You will eliminate the risks of making wrong decisions.
Increased Profitability
MES software will help you earn more money by boosting productivity and ensuring cost efficiency. It will also lead to improved yield and margins. The manufacturing execution system makes your business safe, compliant, and reputable and helps you grow the company and manufacture more considerable product amounts. Altogether, it will increase profits for your food and beverage company.
Streamlined Inventory (Benefit Summary)
Optimized inventory management is another positive aspect of implementing MES software. You will better manage materials and allocate resources, helping you avoid spoilage and financial losses.
Waste Reduction
Unfortunately, the food industry adversely affects the environment in general. Nearly a quarter (26%) of greenhouse gas emissions are caused by food production. Scientific sources also state that food waste, in particular, contributes to 6% of global greenhouse gas emissions.
With MES software, you will improve your waste management and prevent overproduction, which could lead to extra spending. We have the example of Cadbury. The world-renowned confectionery company has realized considerable cost savings through better resource allocation and waste management, contributing to its sustainability goals.
These are some of the benefits of installing MES, and depending on your goals and specifics, it can bring you more advantages. For instance, Nestlé searched for a solution to comply with food safety standards and maintain quality across the factories worldwide. They implemented the manufacturing execution system to manage traceability, safety, and compliance.
MES and Supply Chain Management
Manufacturing Execution Systems (MES) are a cornerstone of effective Supply Chain Management (SCM) in today’s manufacturing industry. By providing real-time visibility into production operations and enabling seamless data exchange with other systems, MES allows manufacturers to control production processes and manage inventory levels with precision. This real-time insight helps optimize supply chain operations, ensuring that raw materials, components, and finished products move efficiently through the entire manufacturing process.
Integrating MES with SCM systems enables manufacturers to improve production efficiency, reduce costs, and enhance customer satisfaction by responding quickly to changes in demand or supply chain disruptions. Advanced technologies such as predictive analytics and machine learning further strengthen MES’s role in SCM, allowing manufacturers to anticipate potential issues, optimize inventory levels, and make proactive decisions. With MES, manufacturers can achieve greater agility, maintain optimal inventory, and ensure that supply chain operations are always aligned with production goals.
Challenges for Implementing MES Systems
While MES is an efficient and beneficial solution, you may still encounter obstacles, and we consider it fair to let you know what can happen so you are fully aware.
Costs
Firstly, MES implementation can be costly, especially for smaller businesses on a tight budget. MES requires significant investment and a large budget for maintenance. The challenge can also include rapid changes in regulations and standards that will lead to additional spending.
Implementation Takes Time
On average, implementing MES can take up to one and a half years. The procedure includes vendor analysis, preparation, customization, and other steps. You need to be patient and take your time to incorporate a solution.
Adapting and Customization
The manufacturing execution system must be fully adjusted to your food business, which demands time, money, and professional expertise. Adapting to current operational needs will also require some effort.
The main MES implementation challenges can be costs, time, and intricate implementation processes. Please remember the list doesn’t aim to discourage you from using MES but to help you be fully prepared.
Choosing a Manufacturing Execution System
MES vendors offer various solutions, but choosing the right option for your type of business is vital. A wrong choice can result in extra financial expenses and additional work.
To overcome this challenge, food manufacturers must consider important factors like production size, financial aspects, technical questions, MES features etc. We also recommend reading app guides like our list of top MES software.
Integration With Other Systems
MES can be integrated with other manufacturing and business systems. However, it can be a challenge. Integrating MES with existing systems, such as ERP, can be difficult, as sometimes the platforms may be incompatible and cause issues, such as errors in data exchange.
To avoid this problem, you must examine the software infrastructure and develop an integration plan. You can also involve technical support. Consider choosing a solution with better integration capabilities.
Besides that, if you still feel like you lack an understanding of the difference between different systems, you can read our MES vs. MOM and ERP vs. MES blogs.
Technical Challenges in MES
MES implementation is a long and technically demanding process. It includes setting up technical infrastructure, such as servers, networks, devices, etc. Imagine how intricate the process can be when you need to implement a comprehensive system throughout the business to make it function properly and catch tiny details in real time.
To avoid costly mistakes, malfunctions, and delays, involve people with advanced MES implementation expertise.
Change Management Challenges in MES Implementation
Implementing a manufacturing execution system will transform your operations and processes.
You may even face resistance from workers who are used to established procedures. You must conduct process reorganization, align stakeholders, establish objectives, etc. It may take time, and failing to familiarize your company with the new system and rules can cause mistakes and delays.
Don't underestimate the importance of change management in MES implementation. Incorporate it to ensure a smooth transition to the new environment and procedures.
Explain the benefits of MES, its importance, and how it can boost the workflow. Guarantee proper training, consider the employees' workload and technical skills, encourage communication, gather feedback, and quickly respond to issues and questions.
Food Safety and Regulatory Compliance
We know how highly regulated the food industry is. In this case, we must ensure that MES complies with standards and that the system helps food manufacturers adhere to food safety and regulatory requirements.
Compliance with food safety standards is crucial from the very beginning of the MES implementation process. You can choose a solution that is tailored to the food industry.
Hiring a professional who will guide you through the process is also a good decision. A specialist will focus on industry-specific aspects and help you adjust your system accordingly.
World Food Brands Implement MES
The best way to demonstrate MES effectiveness is to showcase the world’s leading food and beverage companies that have successfully implemented a manufacturing execution system and helped them elevate their business.
Top brands, such as Mars, Nestle, PepsiCo, and Conagra Brands, have successfully implemented manufacturing execution systems (MES) that have helped them improve operational efficiency, ensure regulatory compliance, and maintain their leading market positions.
This proves that incorporating MES system is a valuable strategy for the company’s success.
Discover FoodReady MES Functionality
If you are a food manufacturer looking for an MES solution, FoodReady software can help you overcome the challenges of MES implementation and bring the best results to your business.
FoodReady cloud-based software allows authorized workers to access daily operations quickly from multiple locations. It provides instant visibility over essential aspects of food production.
FoodReady is equipped with comprehensive monitoring tools and integrated IoT devices that will allow you to control manufacturing processes at different supply chain stages. Monitoring and analytics capabilities will provide cross-functional transparency and enhance data exchange.
FoodReady food safety software will ensure your food safety compliance with local and state regulations. You will also be able to enhance food traceability and meet the new food traceability rule requirements.
We greatly care about quality assurance at FoodReady, so once you implement our solution, you will benefit from diverse quality control and assurance features. You will also worry less about inventory management, recipe formulation, maintenance management, and other significant tools you are looking for.
FoodReady is affordable; you can find the best package with easy implementation and quick training. Our user-friendly interface lets you start working with the MES faster than expected.
FoodReady goes beyond food safety software and combines the functionality of the MES you are searching for. Contact us, and together, we can bring your company to the next level.
Want real-time visibility across your food production process?
See how FoodReady’s MES capabilities simplify compliance and boost efficiency.
Dashboard
Conclusion
Manufacturing execution software (MES) is an indispensable tool for overseeing the whole manufacturing process, from raw materials to finished goods.
Of course, as with any other comprehensive solution, it requires time and money to start working with, and you may postpone implementing it into your business due to high costs, system complexity, preparation procedures, etc. However, MES benefits prevail over the challenges.
The system will save you money and time, provide 100% visibility, help improve food safety compliance, optimize inventory, and manage food traceability. It’s worth a try, as MES will become your long-term investment in your food and beverage company development.
FoodReady software will be a perfect solution if you are looking for affordable and modern manufacturing execution system. We will help you overcome your fears and the most difficult challenges. Book a demo to see FoodReady’s MES functionality in full.
FAQ
What is the difference between MES and ERP?
MES differs from ERP. According to the ISA-95 model, MES and ERP are on different manufacturing levels. MES focuses on manufacturing optimization, while ERP captures a broader scope of functions like HR, finance, sales, etc.
How scalable is the MES?
MES is a highly scalable solution that allows food manufacturers to implement it once and use it as their business grows.
How does MES data enable better decision-making during audits?
MES collects and stores quality data and other essential information for food safety audits. It will allow food businesses to prepare in real-time and access the needed information promptly during the HACCP, GMP, GFSI, FSMA, and other audits.
Is QMS part of MES?
No, they are different systems, but both QMS and MES have quality control as an essential part of each system.
What Is the role of continuous monitoring and improvement in MES adoption?
Continuous monitoring and improvement play a significant role in MES implementation and usage. To avoid further hardships and drawbacks, you should establish monitoring procedures, analyze feedback, and monitor the market and the company's state. Don’t forget about regular improvements and updates to drive continuous improvement.
Is MES a cost-effective solution to reduce scrap?
Even though MES requires investment, it will help cut expenses caused by scrap and waste, thanks to real-time visibility, enhanced quality control, optimized inventory, etc. Moreover, scrap minimization is not the only aspect MES oversees. The solution brings you many benefits and functions, making it a cost-effective idea.
What is the formula for calculating the scrap rate?
You can calculate the scrap rate using a formula: Scrap Rate % = (Number of Discarded Units / Total Production Run) x 100.
What data does MES gather to optimize maintenance?
MES collects equipment condition and performance data, usage rates, and other related information. The software gathers all the data needed to identify maintenance needs, avoid breakdowns, and optimize maintenance processes.
Can MES help with supplier quality management?
Yes. MES helps oversee supplier quality management by providing tools like integration with QMS, supplier traceability, or performance analysis. The system will let you monitor and control incoming materials from suppliers.
What are the future trends in manufacturing execution systems?
Supposedly, there will be more development in AI engagement in MES, broader mobile device availability, sustainability-focused solutions, and more.
What are the regulations for MES?
The FDA and ISO regulate MES.
Is cloud-based MES secure enough for food manufacturers handling sensitive production data?
There may be a misconception that cloud MES is less secure than on-premise. However, it’s not true. Cloud MES software solutions are safe, as they use encryption, multifactor authentication, and security updates to ensure data confidentiality. Finding a reliable provider that adheres to security standards is also essential.
What are the hidden costs of implementing an on-premise MES system?
Food manufacturers pay for hardware upgrades, maintenance, salaries, or license renewals. Securing the software from cyberattacks and other problems also requires additional investment.
Speak with our Expert Consultants
15–30 minutes. We map FoodReady to your process, plug in your real HACCP plan, and show you the auditor view before the call ends.
About the author
Gerry Galloway
Co-Founder, President & CEO
Gerry Galloway is Co-Founder, President & CEO of FoodReady. He has 20+ years of executive leadership across software, traceability, and food and beverage consulting, and previously advised Fortune 500 companies including Kraft, ConAgra, Amazon, and Peet’s Coffee on supply chain optimization.